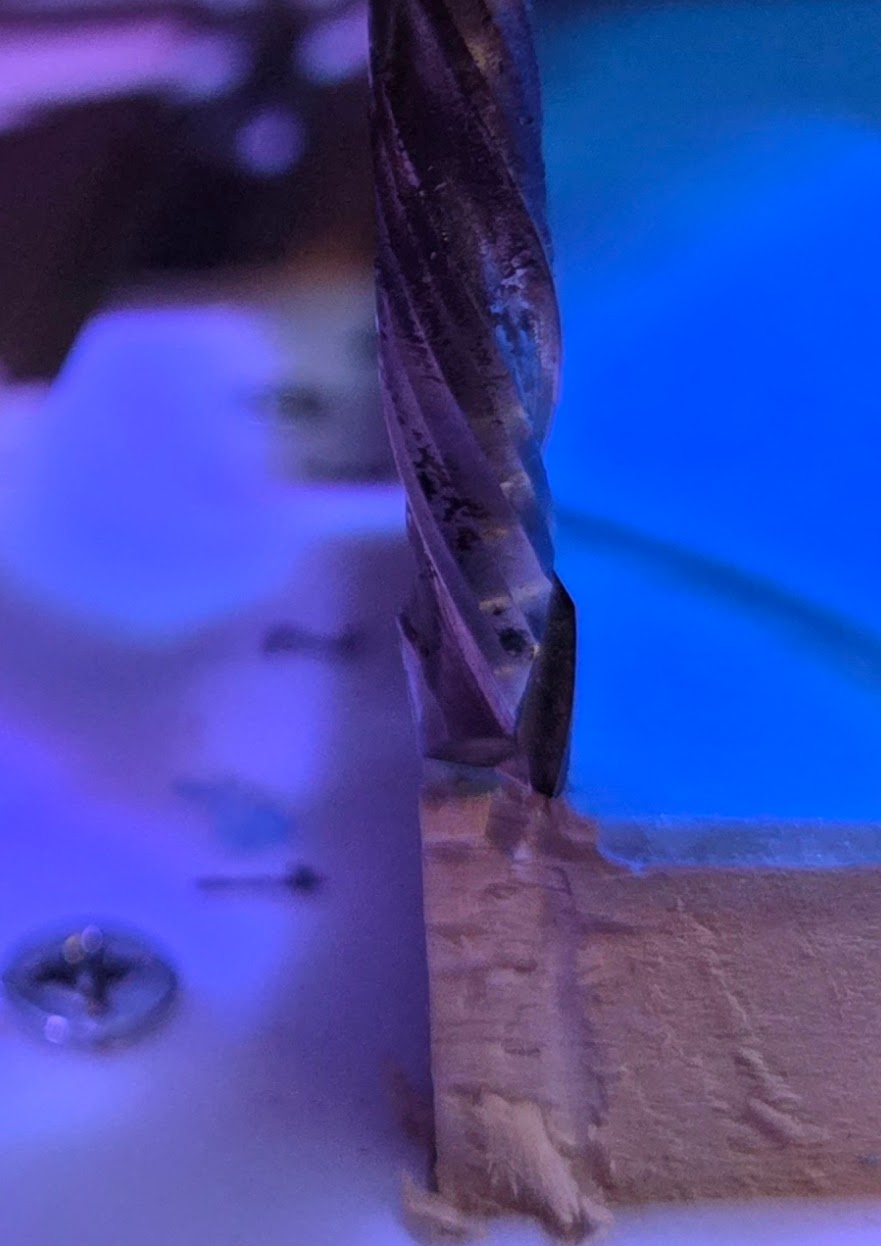
I have had the Auto Zero probe for a couple of years and it has generally functions as expected. XY zero was always set at the center of the bit (both with auto and entering bit diameter). With the latest version of Gsender my XY is set with the edges of the bit lining up with the edge of the material.
I supposed I can jog in either direction 1/2 the diameter of the bit and reset zero but not sure why the change in results.
I have an Xcarve running GRBL 1.1h
$0=10 (Step pulse time, μs)
$1=255 (Step idle delay, ms)
$2=0 (Step pulse invert, mask)
$3=7 (Step direction invert, mask)
$4=0 (Invert step enable pin, boolean)
$5=0 (Invert limit pins, boolean)
$6=0 (Invert probe pin, boolean)
$10=0 (Status report options, mask)
$11=0.020 (Junction deviation, mm)
$12=0.002 (Arc tolerance, mm)
$13=1 (Report in inches, boolean)
$20=0 (Soft limits enable, boolean)
$21=1 (Hard limits enable, boolean)
$22=1 (Homing cycle enable, boolean)
$23=3 (Homing direction invert, mask)
$24=25.000 (Homing locate feed rate, mm/min)
$25=750.000 (Homing search seek rate, mm/min)
$26=250 (Homing switch debounce delay, ms)
$27=5.000 (Homing switch pull-off distance, mm)
$30=1 (Maximum spindle speed, rpm)
$31=0 (Minimum spindle speed, rpm)
$32=0 (Laser-mode enabled as spindle, boolean)
$100=23.403 (X-axis travel resolution, step/mm)
$101=23.403 (Y-axis travel resolution, step/mm)
$102=52.551 (Z-axis travel resolution, step/mm)
$110=8000.000 (X-axis maximum rate, mm/min)
$111=8000.000 (Y-axis maximum rate, mm/min)
$112=600.000 (Z-axis maximum rate, mm/min)
$120=500.000 (X-axis acceleration, mm/sec^2)
$121=500.000 (Y-axis acceleration, mm/sec^2)
$122=500.000 (Z-axis acceleration, mm/sec^2)
$130=750.000 (X-axis maximum travel, mm)
$131=750.000 (Y-axis maximum travel, mm)
$132=100.000 (Z-axis maximum travel, mm)
I have tried with $13=0 with the same results and the same whether probing XYZ or XY only.
ok
[VER:1.1h.20190825:][WWW.PICENGRAVE.COM]
[OPT:V,15,128]
ok